6-Sided CNC Drilling Return Systems: Eliminating Secondary Handling & Stacking
An engineering guide to retrofitting automated loop and under-bed return conveyors on 6-sided CNC drilling machines (Nanxing, KDT, Excitech, Biesse, and Homag). Eliminate rear outfeed catchers, prevent hole chipping, and achieve continuous single-operator boring cycles.
The Hidden Bottleneck Behind High-Speed 6-Sided CNC Borers
Six-sided CNC boring centers—such as the Nanxing NDT series, KDT KD-612 series, Excitech E6, and European counterparts from Biesse and Homag—represent one of the greatest technological leaps in custom furniture manufacturing. In a single continuous clamp cycle, these machines execute all top, bottom, and side system holes, hinge cups, and back-panel routing channels simultaneously.
However, when operated without an automated return conveyor, a severe logistical imbalance occurs at the machine outfeed:
- The Costly Rear Catcher: Because the machine clamps panels and feeds them longitudinally out the rear, an additional dedicated worker must stand at the outfeed discharge to manually catch drilled boards and stack them onto rolling carts.
- Machine Idling During Infeed Scanning: While the rear worker is busy stacking a panel, the infeed operator must walk between pallets, scan the next barcode, and align the raw board. This manual lag leaves the machine’s 20+ drilling spindles idling for up to 40% of the working shift.
- Drill Hole Chipping & Debris Damage: Finished panels exit with fresh dowel holes and back-grooves. When manual workers drag boards off the outfeed table onto metal carts, drill shavings trapped between faces cause surface scratches, and board corners bump raw holes.
[ Traditional Standalone 6-Sided Drilling Flow ]
Infeed Operator ──► [6-Sided CNC Borer] ──► Rear Outfeed Catcher (Extra Worker)
      ▲                                                    │
      └───────── Manual Hand Cart Walking & Sorting ───────┘
[ Automated Loop Return Flow (Single Operator) ]
Infeed Operator ──► [6-Sided CNC Borer] ──► [Automatic Outfeed Lift / Lower]
(Feed & Scan)                                              │
      ▲                                                    ▼
      └────────── Return Roller Bed / Under-Bed Loop ◄─────┘
      * Operator scans next part while current part is boring; zero walking, zero rear catcher
2 Core Return Architectures for 6-Sided Boring Cells
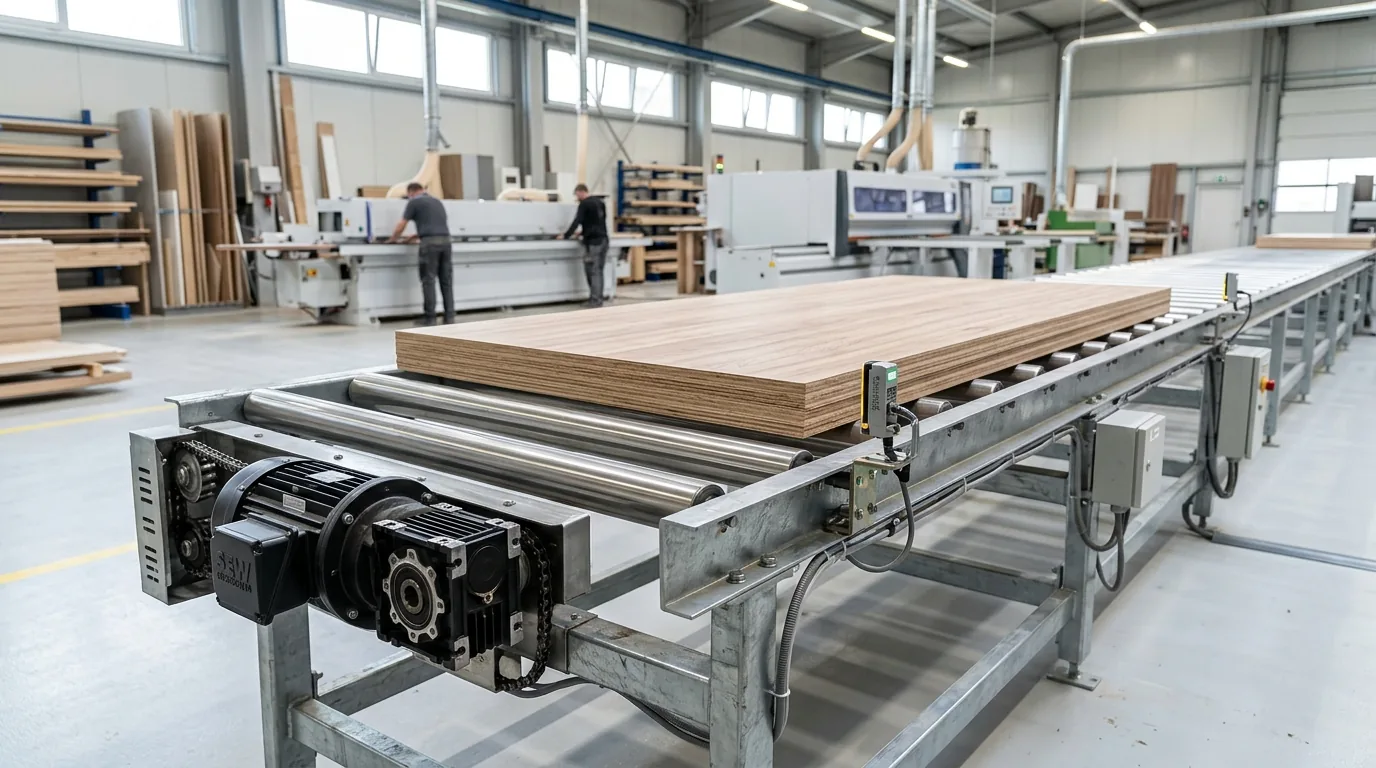
Depending on factory floor dimensions and machine discharge geometry, two automated return configurations deliver single-operator productivity:
1. Lateral Loop Return Conveyor (U-Shape / O-Shape)
Positioned alongside the 6-sided borer. When the panel clears the rear outfeed clamp, pneumatic pop-up cross transfer belts elevate the panel 90° sideways onto an adjacent motorized return roller line. The panel is propelled back to the front infeed table, arriving right at the operator’s fingertips.
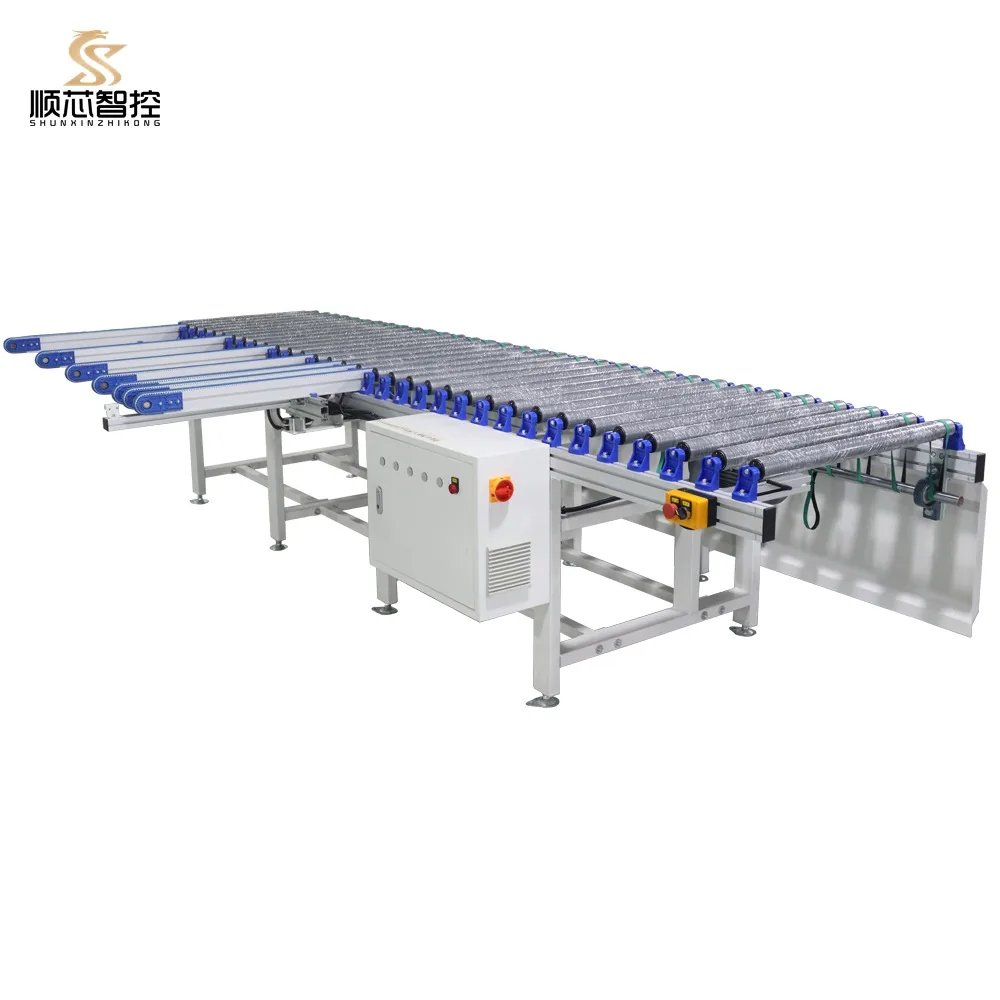
Equipped with independent variable-frequency inverter controls and optical sensors, synchronizing roller speeds with the CNC borer's automatic clamp movement.
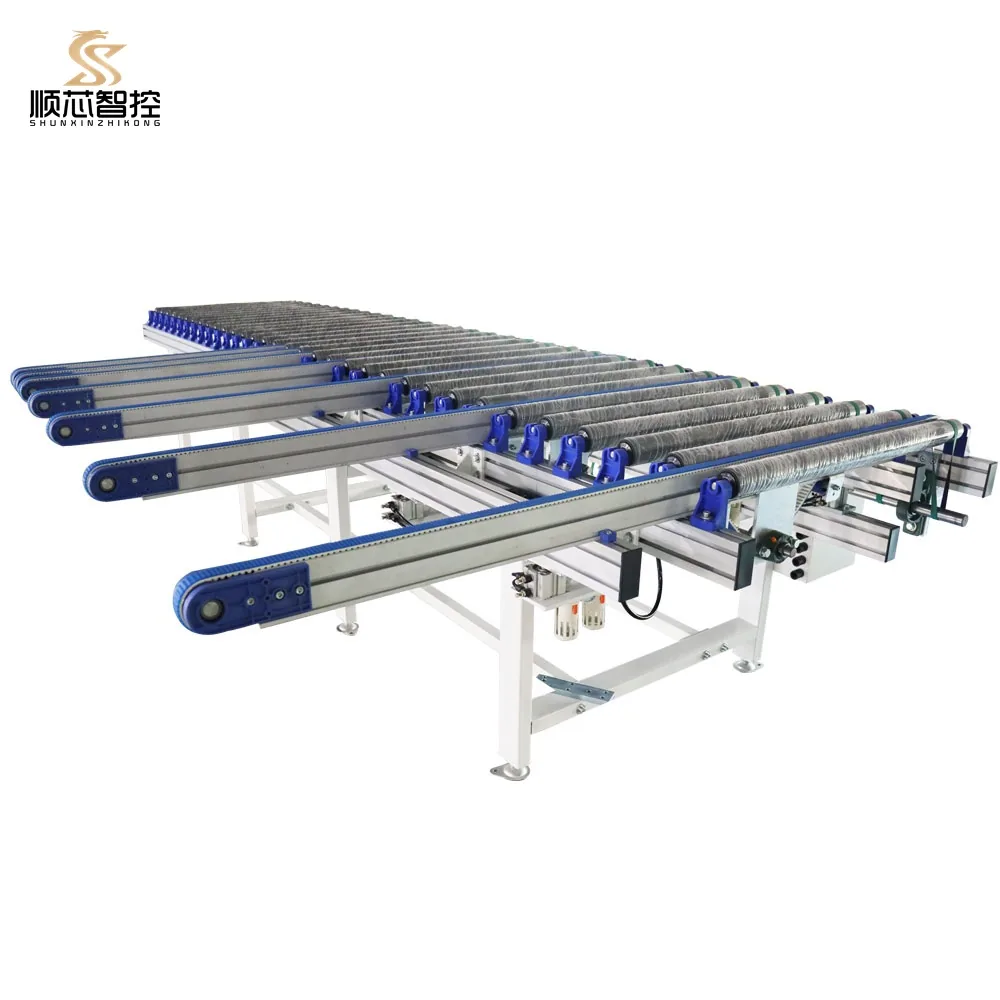
Multi-strand polyurethane timing belts elevate pneumatically at the discharge mouth, shifting finished panels 90° onto the return lane without surface friction.
2. Under-Bed Vertical Lowering Return (Space-Saver)
For workshops with restricted side clearance (less than 2.0 m between machine rows), an under-bed return system lowers the drilled panel vertically at the outfeed and returns it directly underneath the CNC boring machine frame, delivering maximum floor space efficiency.
4-Step Production Protocol for Single-Operator Drilling
Barcode Pre-Scanning & Program Buffering
The operator scans the barcode label on Board B using an overhead wireless optical scanner while Board A is actively drilling inside the machine. The CNC software pre-loads the drilling program instantaneously.
Synchronous Infeed Insertion
As Board A completes its boring cycle and discharges, the operator immediately pushes Board B against the pneumatic infeed reference fence. The machine clamps Board B within 2.5 seconds.
Automated Lateral Outfeed Transfer
Board A triggers an optical sensor at the outfeed roller bed. Pneumatic pop-up belts elevate, shifting Board A onto the return conveyor lane at 28 m/min.
Return Stacking & Quality Verification
Board A arrives on the front air cushion table directly beside the operator. The operator performs a quick visual check on hole depth and stacks Board A onto the finished pallet—all while Board B is drilling.
Global Industrial & GEO Export Standards for CNC Drilling Conveyors
Export machinery must meet strict international technical compliance for seamless integration:
GEO STANDARDS 6-Sided Drilling Regional Compatibility Matrix
- Electrical: 480V / 208V, 60Hz 3-Phase dual-voltage motors
- Standards: UL 508A compliant control panels, NFPA 79 safety circuits
- Economic Impact: Eliminating one \$24/hr rear catcher provides payback in under 3.2 months
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-emerald-400"></span>
    European Union (Germany, Poland, Italy Cabinetry)
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Directives: CE Machinery Directive 2006/42/EC, EN ISO 13849-1 Cat.3 / PL d safety relays</li>
    <li>Energy Standards: IE3 premium efficiency variable-frequency drives, 400V 50Hz</li>
    <li>Data Integration: Barcode interface compatible with imos, TopSolid, and Homag woodWOP</li>
  </ul>
</div>

<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-amber-400"></span>
    Southeast Asia (Vietnam, Malaysia Modular Furniture Plants)
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Power Grid: 380V, 50Hz standard Asian voltage</li>
    <li>Dust Ingress: IP55 totally enclosed fan-cooled drive motors built for high-dust workshop environments</li>
    <li>Throughput Target: Engineered for continuous multi-shift high-volume export cabinet manufacturing</li>
  </ul>
</div>

<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-purple-400"></span>
    Export Packaging & Sea Transit Standards
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Packaging: Solid timber crates compliant with ISPM-15 international export regulations</li>
    <li>Protection: Heavy-duty VCI vapor anti-corrosion barrier with industrial desiccant packets</li>
    <li>Container Efficiency: Modular structural sections fit standard 20GP / 40HQ container space</li>
  </ul>
</div>
Technical Comparison: 6-Sided Boring Operations
| Operational Parameter | Standalone 6-Sided Borer | Borer with Automated Return Conveyor |
|---|---|---|
| Required Manpower | 2 Workers (Infeed + Rear Catcher) | 1 Operator (Continuous Flow) |
| Spindle Operating Efficiency | 55% – 65% (Manual pause lag) | 85% – 92% (Continuous infeed) |
| Average Daily Output (8-hr shift) | 600 – 750 panels | 1,100 – 1,350 panels |
| Face & Hole Scratch Defect Rate | 1.8% (Manual cart friction) | <0.1% (Motorized non-marking rollers) |
| Floor Space Requirement | Large pallet cart staging areas | Compact closed-loop conveyor footprint |
Operating Pro-Tips for CNC Drilling Cells
[!TIP] Position the Barcode Scanner Directly Above Infeed: Mount a fixed industrial barcode camera directly over the infeed roller bed. The camera reads the QR code as the operator places the board on the table, eliminating manual handheld scanner handling.
[!WARNING] Check Roller Clearance for Protruding Dowels: If your 6-sided borer features an automatic dowel insertion unit, ensure the return line’s roller spacing and pop-up belt height accommodate protruding 8 mm or 10 mm wood dowels without snagging.
Summary & Integration Consultation
Pairing your 6-sided CNC drilling machine with an automated return conveyor is the single most effective upgrade to eliminate rear unloading labor, protect finished panel faces, and unlock the machine’s true rated throughput.
Contact our automation engineering team today with your 6-sided borer brand (Nanxing, KDT, Excitech, Biesse, or Homag) and workshop floor layout to receive custom 3D integration blueprints and an itemized CIF export quote.
All automated loop return procedures and electrical sensor alignments must adhere to standard workshop lockout-tagout (LOTO) protocols and host machinery manufacturer guidelines. Shunxin equipment includes universal dry-contact interlocks to ensure immediate emergency stop response across synchronized production lines.
Need a Custom Layout Drawing & Quotation for Your Workshop?
Send us your workshop dimensions or CAD floor plan. Our mechanical engineers will deliver a synchronized layout proposal and payback calculation within 24 hours.