How to Prevent Thin Panel Deformation During High-Speed Vacuum Gantry Transfer
An engineering guide to handling flexible 5mm, 6mm, and 9mm wardrobe backboards, drawer bottoms, and acoustic panels without bowing, creasing, or dropping during high-speed automated gantry crane transfer. Master multi-zone sponge arrays and S-curve servo acceleration.
The Physics of Thin Panel Handling: Why Flexible Boards Warp and Drop
In custom wardrobe manufacturing, commercial flat-pack cabinetry, and acoustic wall cladding production, thin engineered wood panels—specifically 5 mm to 9 mm MDF, HDF, and flexible birch plywood—are among the most difficult materials to automate.
Unlike rigid 18 mm (3/4 in) structural cabinet carcasses, thin sheets possess very low flexural modulus:
- The “Bowing Trampoline” Effect: When conventional gantry loaders utilize 4 or 6 widely spaced round vacuum cups, the central span and unsupported corners of a 2440 × 1220 mm thin sheet droop by up to 120 mm under gravity.
- Vacuum Leakage from Peeling Moments: As a warped thin board accelerates horizontally, air drag lifts the unsupported drooping perimeter. This exerts severe peel forces on peripheral suction cups, breaking the vacuum seal and causing the entire panel to crash onto conveyor beds.
- Permanent Core Creasing: When high vacuum pressure (-85 kPa) is applied through small-diameter round cups on damp 5 mm fiberboard, the concentrated atmospheric force leaves permanent circular dimples and core delamination rings on the decorative paper laminate.
[ Problem: Widely Spaced Round Cups ]
      ▲ Lifting Force              ▲ Lifting Force
   [Round Cup]                  [Round Cup]
───────┬──────────────────────────────┬───────
       ▼ Drooping Center & Corners    ▼ Drooping Corners
  * Severe flexural sag, air leakage at corners, high drop risk at >30 m/min
[ Solution: Distributed Sponge Matrix & Co-Planar Grid ]
  ▲       ▲       ▲       ▲       ▲       ▲       ▲
[Sponge] [Sponge] [Sponge] [Sponge] [Sponge] [Sponge] [Sponge]
───────────────────────────────────────────────────────────── (Flat Panel)
  * Uniform distributed suction, zero perimeter sag, safe transfer at 60 m/min
4 Engineering Solutions to Eliminate Thin Panel Deformation
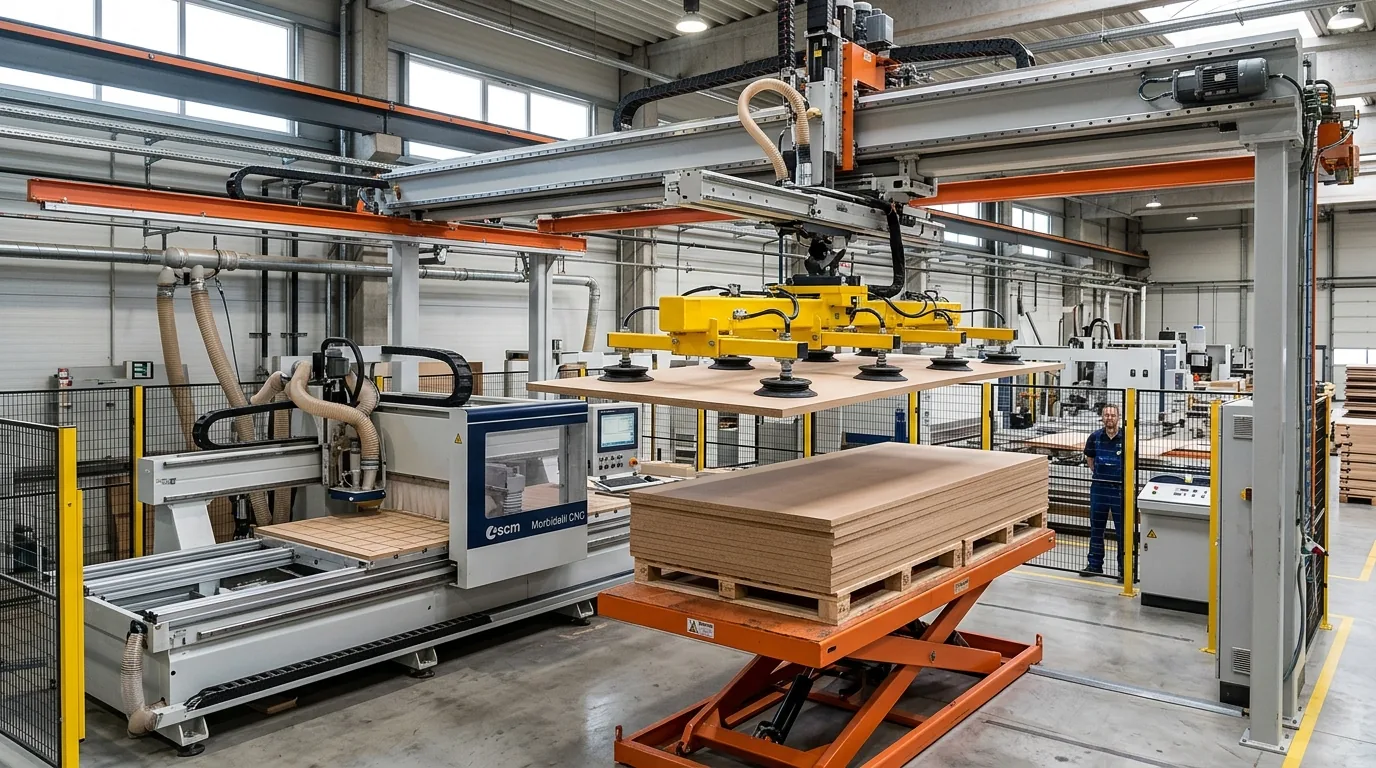
To enable automated gantry systems to run at full speeds (up to 60 m/min) while handling thin flexible panels, our engineering team implements four synchronized mechanical and software controls:
1. High-Density Closed-Cell EPDM Foam Matrix
Instead of discrete round cups, high-speed gantries utilize continuous closed-cell sponge vacuum grids. Micro-valved check channels activate only the surface area sealed by the workpiece. The continuous contact line supports the thin sheet like an air mattress, distributing holding pressure evenly across the entire face.
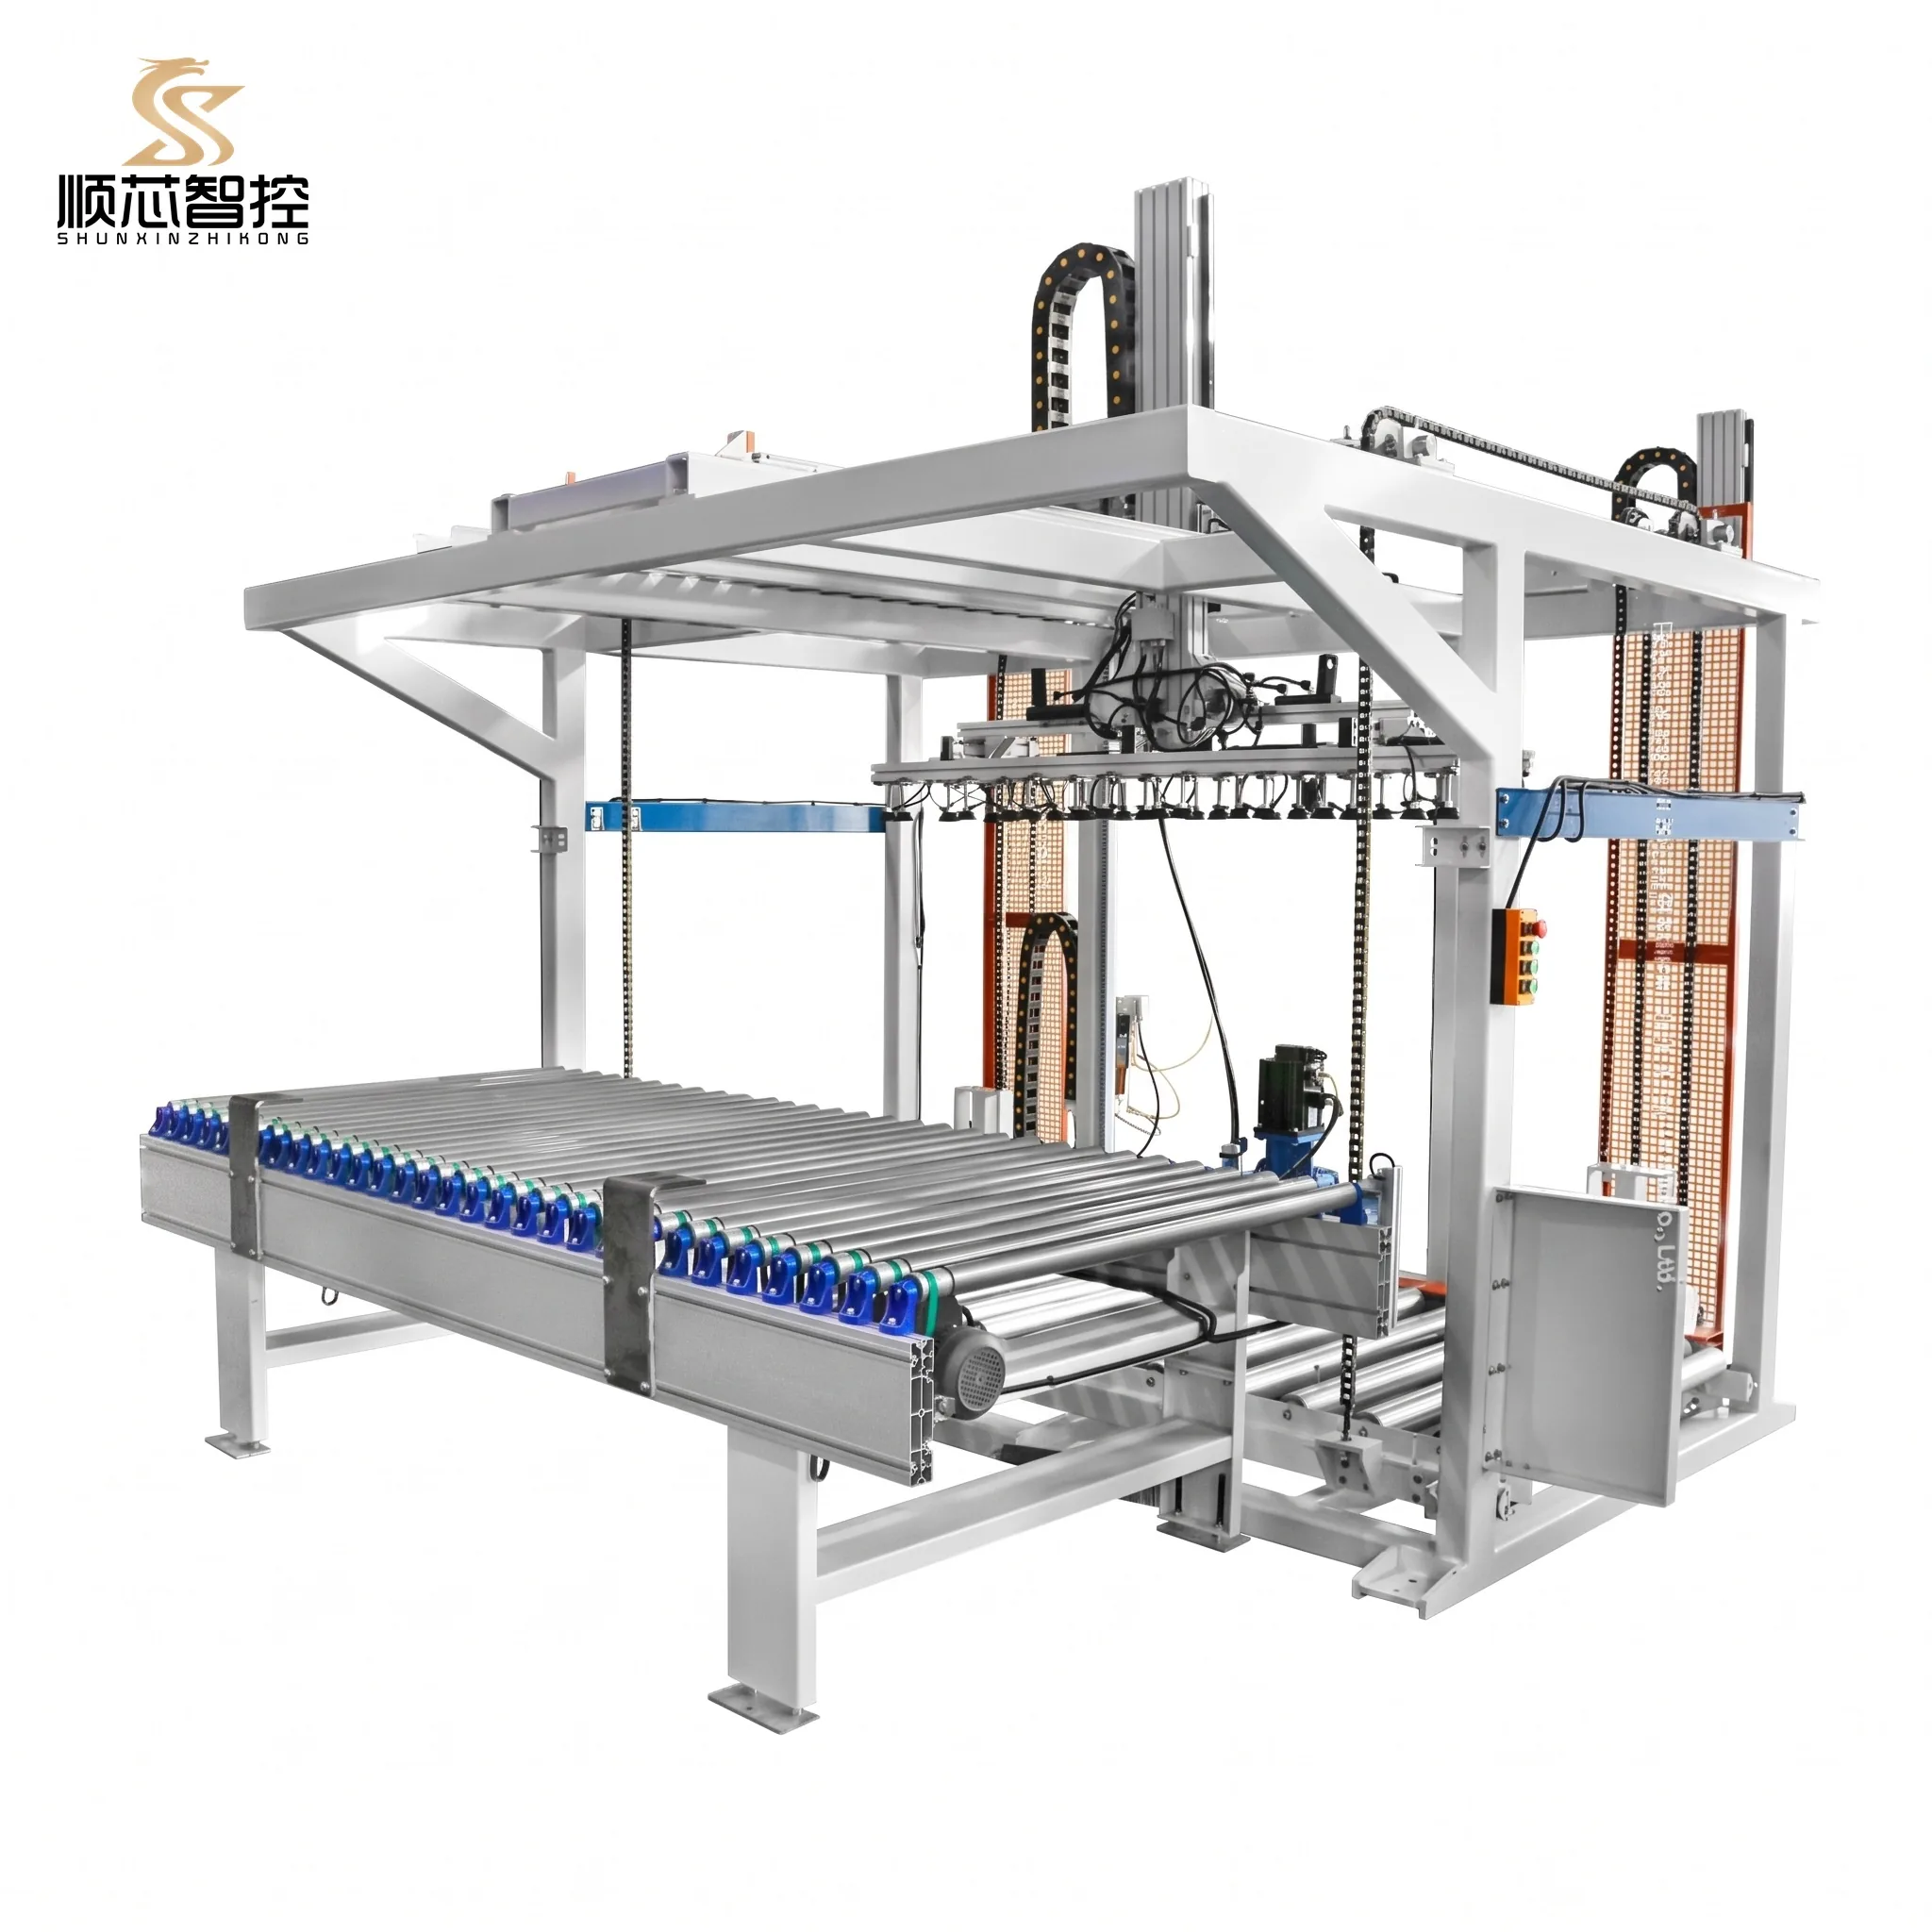
Four heavy structural columns eliminate mechanical vibration and gantry frame twist during rapid acceleration, ensuring vacuum beams remain coplanar within ±0.3 mm.
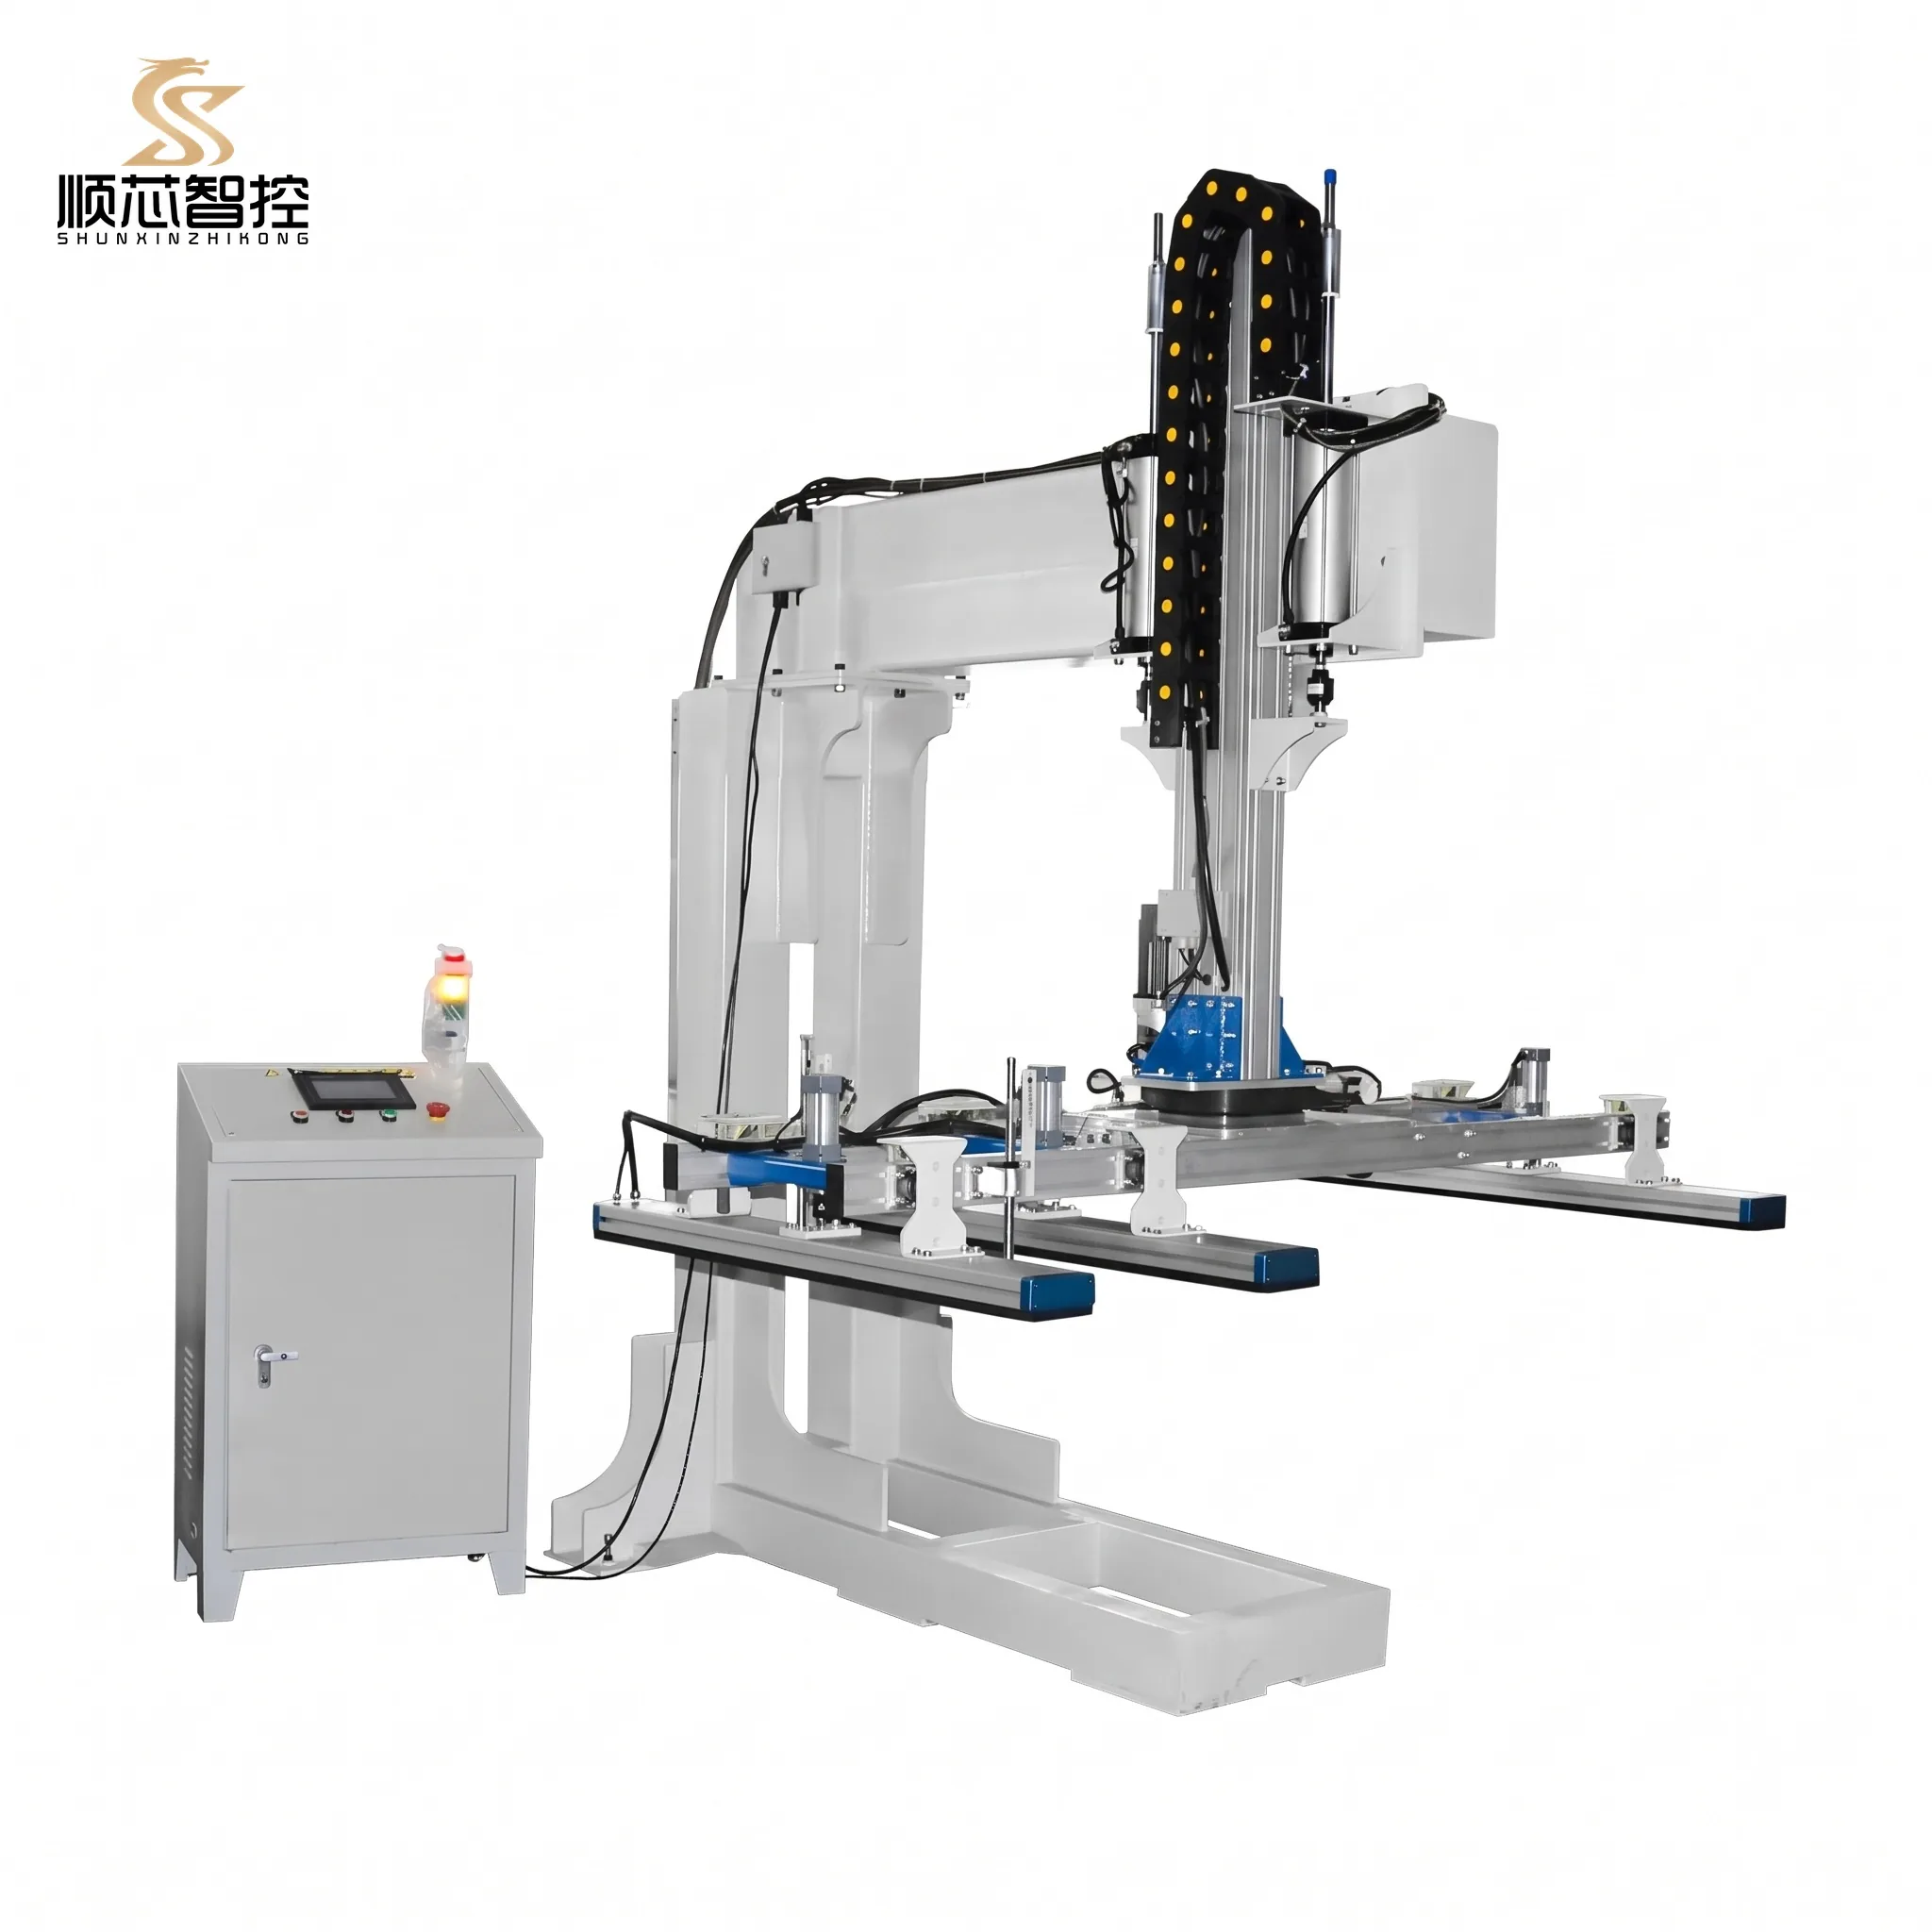
High-velocity lateral air nozzles blow clean compressed air between thin stacked sheets during initial lift, breaking vacuum adhesion between stacked boards.
2. S-Curve Jerk-Free Servo Acceleration
Abrupt starts and stops cause flexible panels to whip violently like a flag in high wind. The servo drive firmware programs a quintic S-curve motion profile. Peak acceleration is capped at 1.8 m/s² with controlled jerk derivatives, eliminating dynamic oscillation during gantry travel.
3. Progressive Edge-to-Center Vacuum Sequencing
When lifting thin sheets off a flat pallet stack, atmospheric vacuum between the two polished surfaces creates intense suction adhesion (often exceeding 500 kg of resistive pull). The gantry tilts the leading row of suction cups 3° upward first, introducing air under the board to gently peel it before the main vertical lift.
4. Dynamic Height-Tracking Infeed Scissor Lift
To minimize vertical drop distances and limit mechanical impact, an optical laser sensor monitors the top of the board stack. A hydraulic scissor lift table automatically indexes the top sheet within a precise 30 mm pick window.
Technical Comparison: Thin Panel Handling Methods
| System Parameter | Standard Concentrated Cups | Distributed Sponge Matrix | Progressive Tilt Vacuum Beam |
|---|---|---|---|
| Max Panel Droop on 6mm MDF | 80 mm – 120 mm (Severe Sag) | <10 mm (Coplanar) | <5 mm (Near Perfect Flat) |
| Double-Sheet Lifting Risk | High (Atmospheric Adhesion) | Medium | Zero (Pneumatic Air Knife) |
| Max Safe Gantry Speed | 22 m/min (Slowed for safety) | 45 m/min | 60 m/min |
| Surface Indentation Marks | Common on soft lacquers | Zero (Closed-Cell EPDM) | Zero (Silicone Bellows) |
| Suction Response Time | 0.8 sec | 0.3 sec | 0.25 sec |
Global Industrial & GEO Export Standards for Thin Panel Automation
Export furniture factories worldwide process thin panels under regional manufacturing standards:
GEO STANDARDS Regional Technical Compatibility Matrix
- Electrical: 480V / 208V, 60Hz 3-Phase dual-voltage motors
- Standards: UL 508A compliant control panels, NFPA 79 safety circuits
- Board Sizes: Optimized for 4ft × 8ft (1220 × 2440 mm) thin drawer bottom sheets
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-emerald-400"></span>
European Union (Poland, Germany, Italy Flat-Pack)
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Directives: CE Machinery Directive 2006/42/EC, EN ISO 13849-1 Cat.3 / PL d safety interlocks</li>
<li>Energy Efficiency: IE3 premium efficiency servo drives and vacuum blowers, 400V 50Hz</li>
<li>Noise: Quiet vacuum blowers with acoustic dampening (<70 dB(A))</li>
</ul>
</div>
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-amber-400"></span>
Southeast Asia (Vietnam, Malaysia Plywood Mills)
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Power Grid: 380V, 50Hz standard Asian voltage</li>
<li>Moisture Resistance: Tropicalized closed-cell EPDM foam impervious to high factory humidity</li>
<li>High-Duty Cycle: Engineered for continuous 24/7 export manufacturing shifts</li>
</ul>
</div>
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-purple-400"></span>
Export Packaging & Sea Transit Standards
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Packaging: Solid timber crates compliant with ISPM-15 international export regulations</li>
<li>Protection: Multi-layer vacuum foil barrier with industrial desiccant packets</li>
<li>Container Efficiency: Modular structural beams fit standard 40HQ container space</li>
</ul>
</div>
Maintenance & Operating Pro-Tips
[!TIP] Clean Vacuum Sponge Foam Weekly: Microscopic sawdust fibers can build up within the porous foam surface. Blow out sponge arrays with a clean compressed air gun weekly to maintain maximum vacuum air permeability.
[!WARNING] Check Air-Knife Angle on Sticky Lacquered Backboards: If thin boards stick together due to static charge or sticky lacquer, adjust the side air-knife nozzle angle to 15° pointing directly at the top seam. This ensures instant aerodynamic separation.
Conclusion & Project Consultation
Handling flexible thin boards at high production speeds requires a disciplined engineering approach combining distributed sponge vacuum beams, peeling sequence lifters, and smooth S-curve servo motion. By eliminating board sagging and vacuum leakage, furniture manufacturers achieve reliable, continuous automation across their thinnest product lines.
Contact our material handling specialists today with your board thickness, dimensions, and cycle targets for custom 3D simulation layouts and turnkey export quotations.
All automated loop return procedures and electrical sensor alignments must adhere to standard workshop lockout-tagout (LOTO) protocols and host machinery manufacturer guidelines. Shunxin equipment includes universal dry-contact interlocks to ensure immediate emergency stop response across synchronized production lines.
Need a Custom Layout Drawing & Quotation for Your Workshop?
Send us your workshop dimensions or CAD floor plan. Our mechanical engineers will deliver a synchronized layout proposal and payback calculation within 24 hours.