KDT Edge Bander Return Line Retrofit: Maximizing Output with 1 Operator
Complete engineering and operational guide for retrofitting KDT edge banders (KE-365, KE-395, KE-396, KE-495, and KE-688) with an automated powered return loop. Eliminate 2 outfeed catchers, synchronize PLC sensor triggers, and boost daily panel throughput by 40%.
The Bottleneck on High-Speed KDT Edge Banding Lines
KDT Machinery edge banders (including popular models such as the KE-365, KE-395, KE-495, and high-speed KE-688) are recognized globally for their rugged track feeds and consistent sealing speeds of 18 to 26 m/min. However, when operating as standalone machines, their high output creates an immediate manual logistics logjam:
- Severe Outfeed Fatigue: Large wardrobe panels (e.g., 2400 × 600 × 18 mm) exiting at 23 m/min require two workers standing in continuous posture strain just to catch, turn, and place panels on return carts.
- Edge Chipping on Corner Drops: Manual workers catching heavy panels frequently bump raw corners against outfeed metal lips or adjacent boards on the trolley, leading to costly PVC/PUR tape rework.
- Paced by Human Fatigue, Not Machine Speed: Even if your KDT machine can process 2,200 panels a shift, production typically falls to 1,300 panels because manual catchers need frequent rest breaks.
Technical Integration & Retrofit Architecture
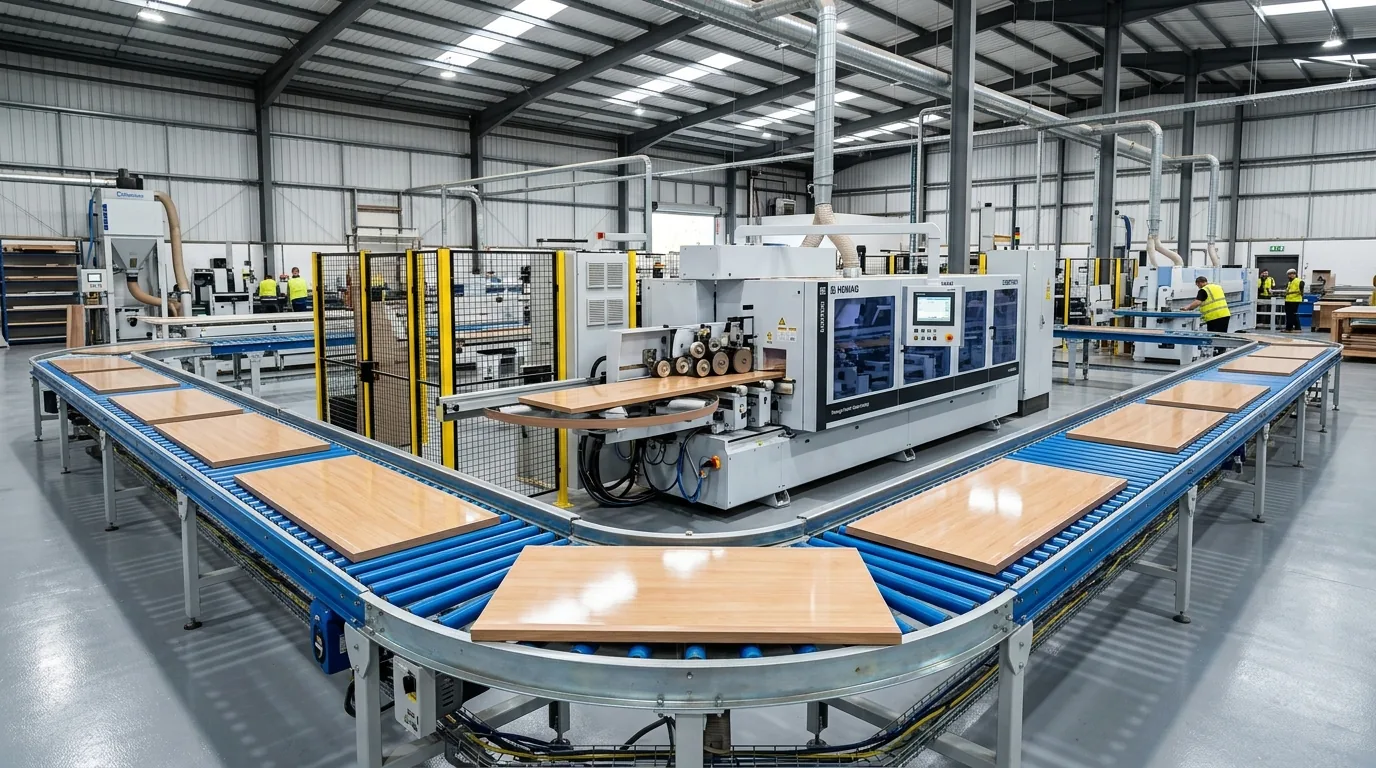
Retrofitting an aftermarket automated return conveyor to a KDT machine does not require modifying the factory warranty or internal PLC programming of the KDT unit. The return system functions as an autonomous, self-synchronized slave cell using smart optical sensors and dry-contact safety interlocks.
1. Mechanical Docking & Height Synchronization
- KDT Track Height: Standard KDT outfeed track height measures approximately 900 mm (±25 mm) from the finished factory floor.
- Receiving Bed Leveling: The return conveyor’s initial transition roller bed is adjusted to 898 mm (a 2 mm drop). This ensures panels transition onto the return system smoothly by gravity without scratching delicate bottom face coatings or catching on tape overhangs.
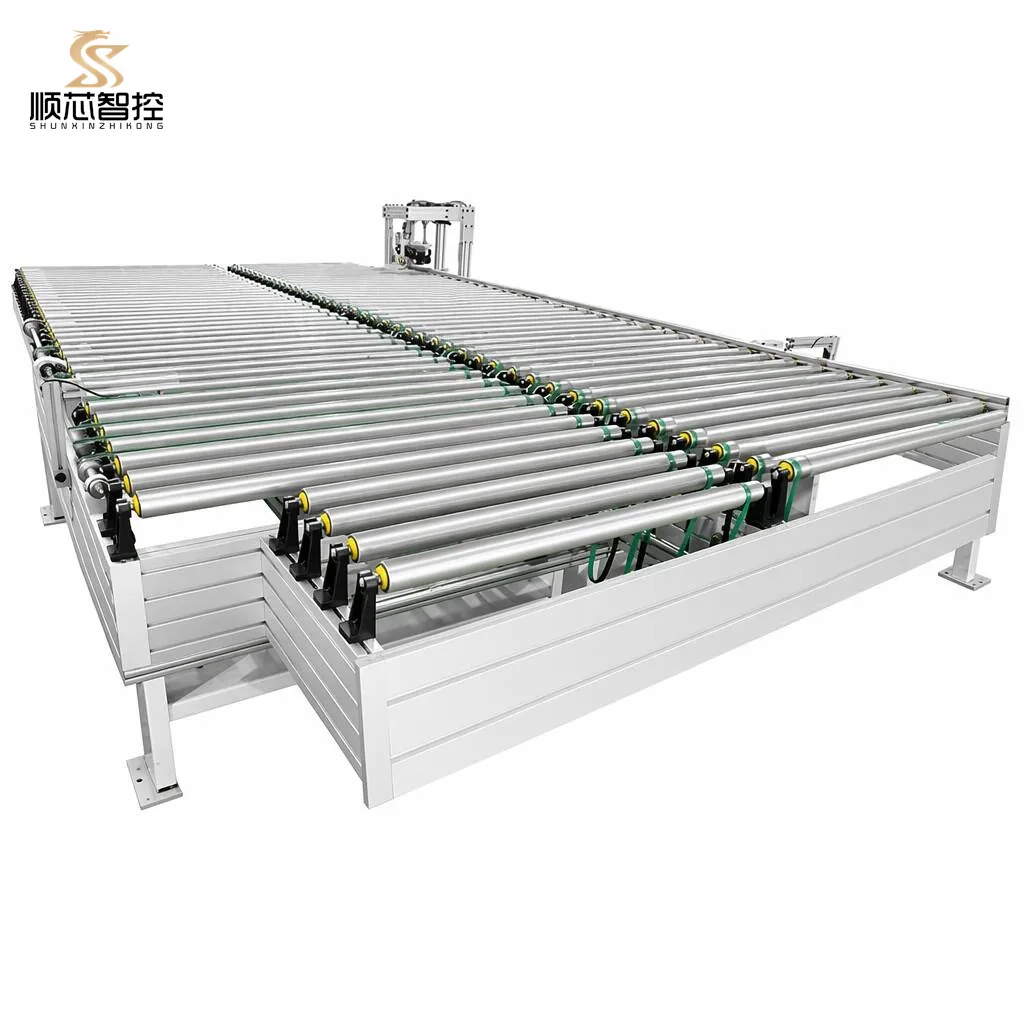
Mounted directly at the KDT outfeed. When the panel clears the outfeed press roller, photoelectric sensors fire the pneumatic cylinder, lifting polyurethane belts to shift the panel 90° sideways.
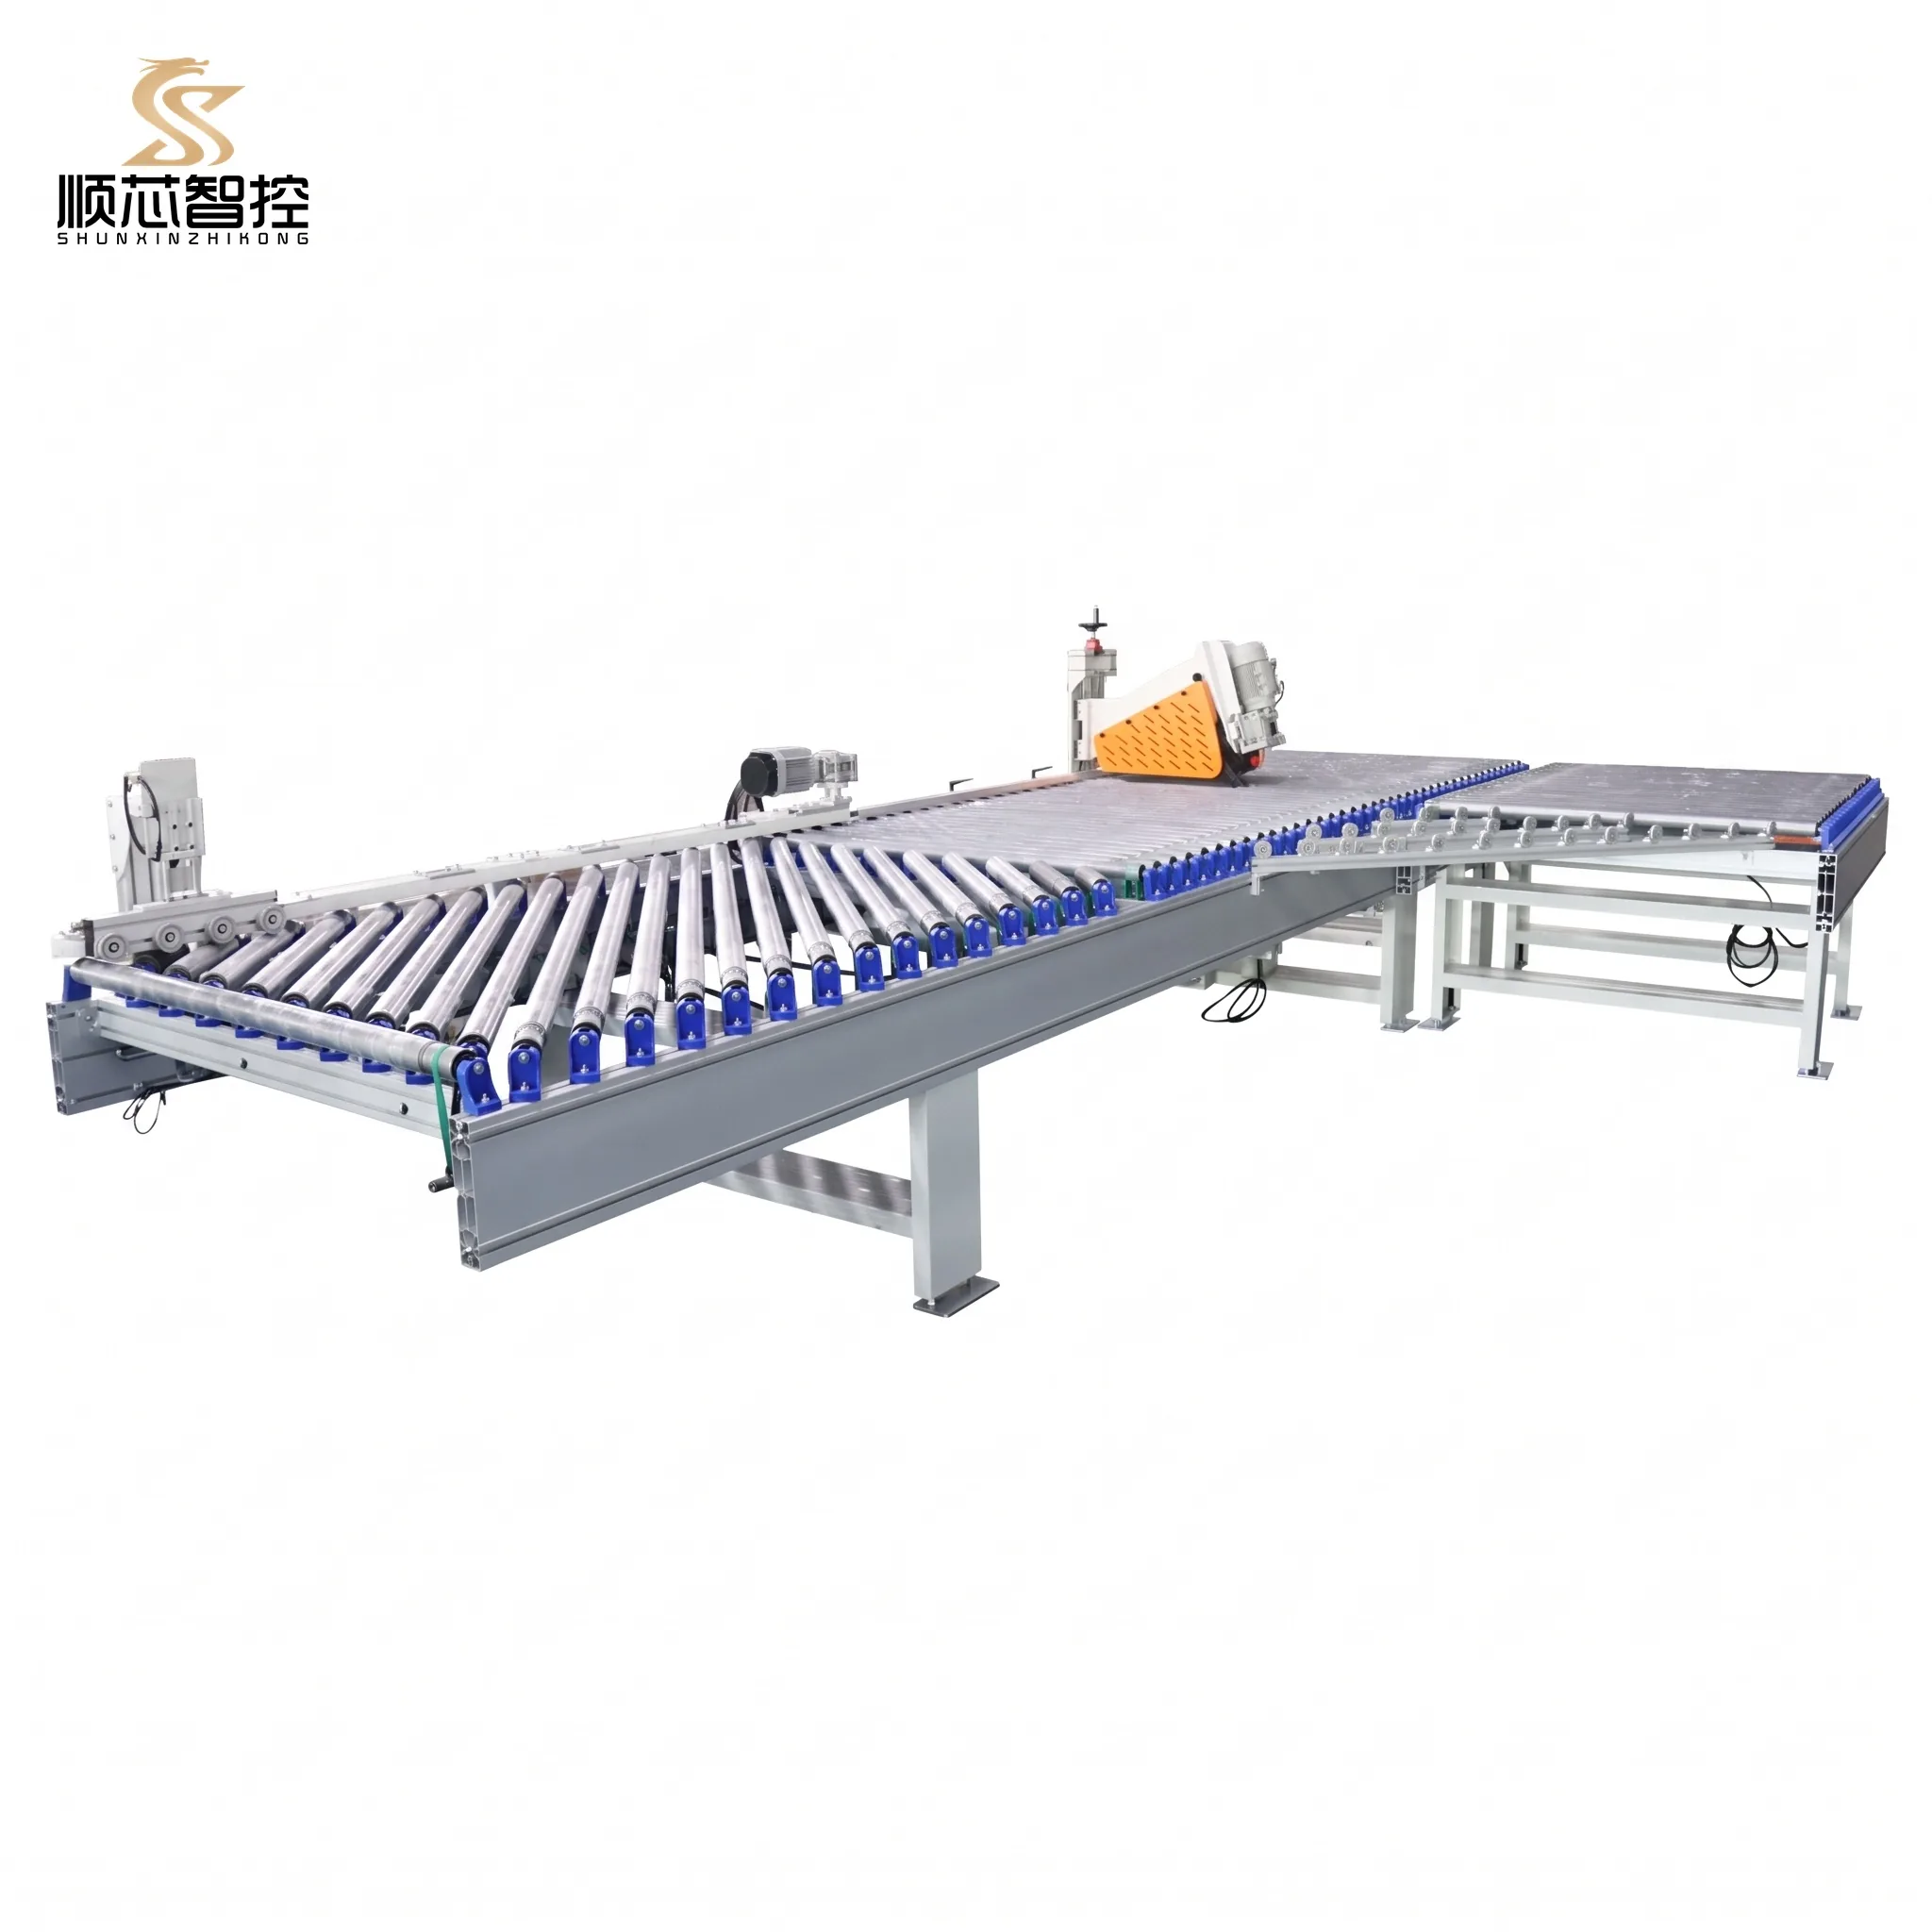
Angled conical polyurethane rollers automatically push returned boards against the reference guide fence, delivering perfectly aligned panels back to the operator's hands.
4-Step Onsite Retrofit Protocol for KDT Units
Completing a seamless KDT retrofit follows a precise engineering sequence:
Floor Space Survey & Clearance Verification
Verify a minimum clear working corridor of 2.6 m to 3.0 m parallel to your KDT machine frame. Mark chalk lines indicating conveyor frame anchors and power drop locations.
Docking & Height Calibration
Roll the receiving module into position directly facing the KDT outfeed chute. Level all support legs using a digital spirit level, locking jam nuts at 898 mm elevation.
VFD Speed & Sensor Timing Calibration
Set the return line inverter to 1.2× the KDT feed speed (e.g., if KDT runs at 20 m/min, set return to 24 m/min). Adjust retroreflective optical sensor sensitivity to trigger belt lift when the tail of the panel clears the outfeed by 100 mm.
Dry Contact E-Stop Integration
Wire the emergency stop safety circuit between the return conveyor and KDT control cabinet. Hitting any emergency button on either machine immediately halts both track feed and return rollers.
Global Industrial & GEO Export Standards for KDT Users
KDT machinery is exported extensively to furniture producers across Southeast Asia, North America, the Middle East, and Eastern Europe. Our retrofit return lines comply with regional factory criteria:
GEO STANDARDS Regional Compatibility & Electrical Compliance
- Motors: 480V / 208V, 60Hz 3-Phase dual-voltage windings
- Controls: UL 508A certified panels, Schneider contactors, NFPA 79 safety wiring
- ROI Advantage: Payback in 2.1 months based on \$25/hr operator labor elimination
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-emerald-400"></span>
    Europe & Eastern Europe (Poland, Czechia, UK)
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Motors: 400V, 50Hz with IE3 premium energy efficiency rating</li>
    <li>Safety: CE Conformity, EN ISO 13849-1 dual-channel safety relays</li>
    <li>Documentation: Full English/German pneumatic schematics and risk assessments</li>
  </ul>
</div>

<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-amber-400"></span>
    Southeast Asia (Vietnam, Malaysia, Indonesia KDT Users)
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Motors: 380V, 50Hz 3-Phase standard Asian grid configuration</li>
    <li>Climate Resistance: High-humidity tropicalized polyurethane belts and anti-rust plating</li>
    <li>Fast Delivery: Direct container shipments to Ho Chi Minh / Port Klang in 7-12 days</li>
  </ul>
</div>

<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
  <div class="font-bold text-white mb-1 flex items-center gap-2">
    <span class="w-2 h-2 rounded-full bg-purple-400"></span>
    Latin America & Nearshoring (Mexico, Brazil)
  </div>
  <ul class="space-y-1 text-slate-400 list-disc list-inside">
    <li>Motors: Dual-frequency 220V/440V 60Hz adaptation</li>
    <li>Packaging: Heavy-duty ISPM-15 wooden crating with desiccants for sea transit</li>
    <li>Support: Remote video commissioning and 24/7 bilingual technical assistance</li>
  </ul>
</div>
Retrofit Compatibility Matrix by KDT Machine Model
| KDT Model | Max Feed Speed | Recommended Return System | Turning Mechanism | Expected Daily Output (8 hr) |
|---|---|---|---|---|
| KE-365 / 365J | 20 m/min | SX-370S Standard U-Return | Air Flotation Ball Table | 1,400 - 1,700 Panels |
| KE-395 / 395J | 23 m/min | SX-370L Extended U-Return | High-Pressure Air Float Bed | 1,800 - 2,100 Panels |
| KE-495 / 496 | 26 m/min | SX-450HD Synchronized Return | Dual-Row Powered Rollers + Air Table | 2,200 - 2,600 Panels |
| KE-688 High-Speed | 30 m/min | SX-500 Heavy-Duty High-Speed Cell | Pop-Up Servo Belts + Conical Oblique | 2,600 - 3,200 Panels |
Operator Pro-Tips for KDT Cell Optimization
[!TIP] Offsetting Board Feeding Gaps: Train your infeed operator to load panels with a consistent 200 mm gap. The return conveyor’s 1.2× speed differential ensures that as Board 1 is returning on the outer track, the operator is already feeding Board 2, maintaining 100% spindle utilization without pauses.
[!WARNING] Check Optical Sensor Dust Accumulation: Sawdust and trimming chips from the KDT end-trimming and corner-rounding units can settle on the return line’s photoelectric sensors. Always wipe optical lenses with a dry cloth during morning shift startup to prevent false triggering.
Summary & Technical Consultation
Retrofitting an automated return conveyor onto your existing KDT edge bander is the fastest way to double machine productivity while reducing labor overhead. Rather than investing in a second edge bander, maximizing your current KDT machine’s continuous throughput delivers immediate bottom-line cash flow.
Contact our technical application specialists with your KDT machine serial number, workshop floor dimensions, and electrical requirements for a comprehensive 3D layout plan and turnkey delivery quotation.
All automated loop return procedures and electrical sensor alignments must adhere to standard workshop lockout-tagout (LOTO) protocols and host machinery manufacturer guidelines. Shunxin equipment includes universal dry-contact interlocks to ensure immediate emergency stop response across synchronized production lines.
Need a Custom Layout Drawing & Quotation for Your Workshop?
Send us your workshop dimensions or CAD floor plan. Our mechanical engineers will deliver a synchronized layout proposal and payback calculation within 24 hours.