Top 5 Causes of High-Gloss Panel Scratches in Edge Banding and How to Eliminate Them
An engineering guide to eliminating handling scratches, micro-swirls, and clamp dents on premium high-gloss acrylic, PET, and UV lacquer panels. Discover air-flotation gliding, soft silicone vacuum flippers, and polyurethane roller protocols that cut rework costs by 95%.
The High Financial Cost of Surface Micro-Scratches
In high-end kitchen cabinetry, luxury wardrobe manufacturing, and architectural wall panel fabrication, high-gloss acrylic, UV-cured mirror lacquers, and ultra-matte PET films represent the highest-margin product lines. However, these mirror-finish surfaces are notoriously vulnerable during edge banding and panel turning:
- No Spot-Repairing Allowed: Unlike solid wood or standard melamine, a hairline scratch on a 1.0 mm co-extruded acrylic door face cannot be buffed out without leaving visible optical distortion. The entire panel must be scrapped and re-routed.
- Massive Material Value Loss: A single finished high-gloss door panel costs between $45 and $95 USD in raw core substrate, primer, acrylic sheet, PUR hotmelt adhesive, and zero-joint laser tape. Scrapping just 3 to 5 panels per shift drains over $4,500 to $8,000 monthly.
- Delayed Order Shipments: Custom kitchen orders require matched grain and uniform batch hue. One scrapped door holds up the entire flat-pack delivery schedule, incurring client penalty fees.
The Top 5 Root Causes of High-Gloss Panel Scratches
Through hundreds of plant diagnostic audits across North America, Europe, and Asia, our engineers identified the 5 primary failure points in panel transfer:
[ Traditional Manual Flip Trap ]
Manual Worker ──► Hard Metal Outfeed Lip ──► Trapped Sawdust Grinds Face ──► Scrap Panel
      │
      └───────── Pinch Point: Hard Rubber Clamps Leave Pressure Dents
[ Zero-Friction Automated Protocol ]
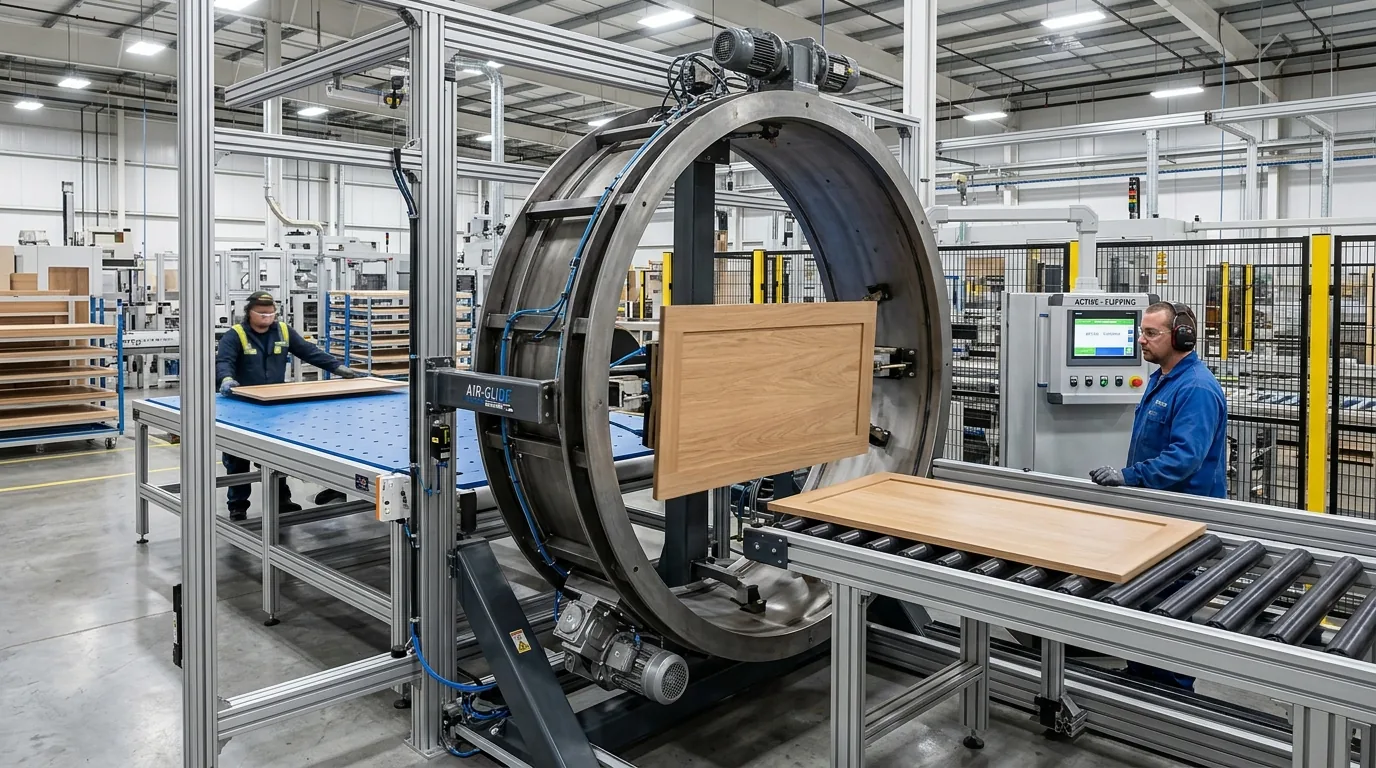
[Edge Bander] ──► [Centrifugal Air Cushion Bed] ──► [Soft Belt 180° Turnover] ──► Flawless Surface
      │
      └───────── 0.5mm Air Micro-Film Suspends Board with Zero Direct Table Contact
1. Trapped Fine Sawdust on Solid Transfer Tables
When an edge bander’s top and bottom trimming units sever excess PVC or ABS tape, fine plastic shavings and MDF dust settle onto metal support tables. When an operator slides a high-gloss panel across this surface, the microscopic particles act like 120-grit sandpaper, scoring long linear scratches into the lacquer.
2. Manual Torso Twisting and Outfeed Corner Dropping
When two outfeed workers manually catch an exiting 2.4 m door, one worker often loses grip, allowing the panel corner to strike the outfeed apron or scrape against the adjacent panel on the transport cart.
3. Hard Mechanical Clamps on Traditional Flippers
Older pneumatic butterfly flippers use rigid rubber or nylon mechanical clamps. The compressive force required to hold a 35 kg panel leaves localized pressure dimples and ring marks on soft PET films.
4. Rigid Unshielded Roller Conveyor Tops
Bare steel rollers or low-durometer recycled rubber rollers pick up metal filings and chip debris, imprinting repetitive ring blemishes every roller revolution.
5. Static Electricity Attracting Abrasive Particulates
High-gloss acrylic sheets generate high triboelectric charges (often exceeding 15 kV) during high-speed edge banding trimming. This static charge magnetically draws airborne carbide saw dust directly onto the panel face right before manual stacking.
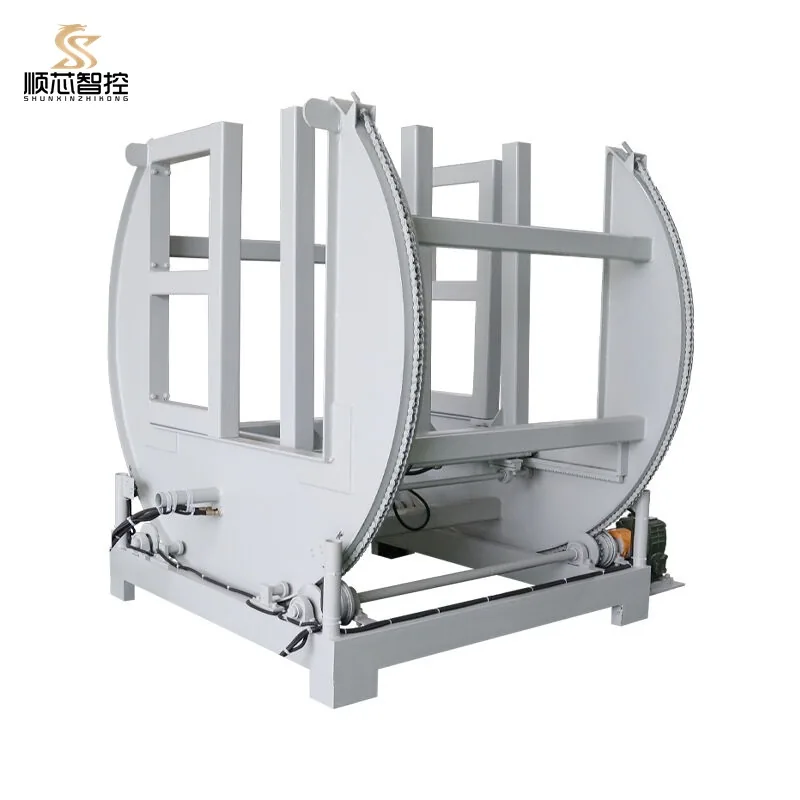
Twin high-friction non-marking food-grade PU belts sandwich the panel under distributed pneumatic pressure, smoothly executing 180° inversions without localized clamp stress.
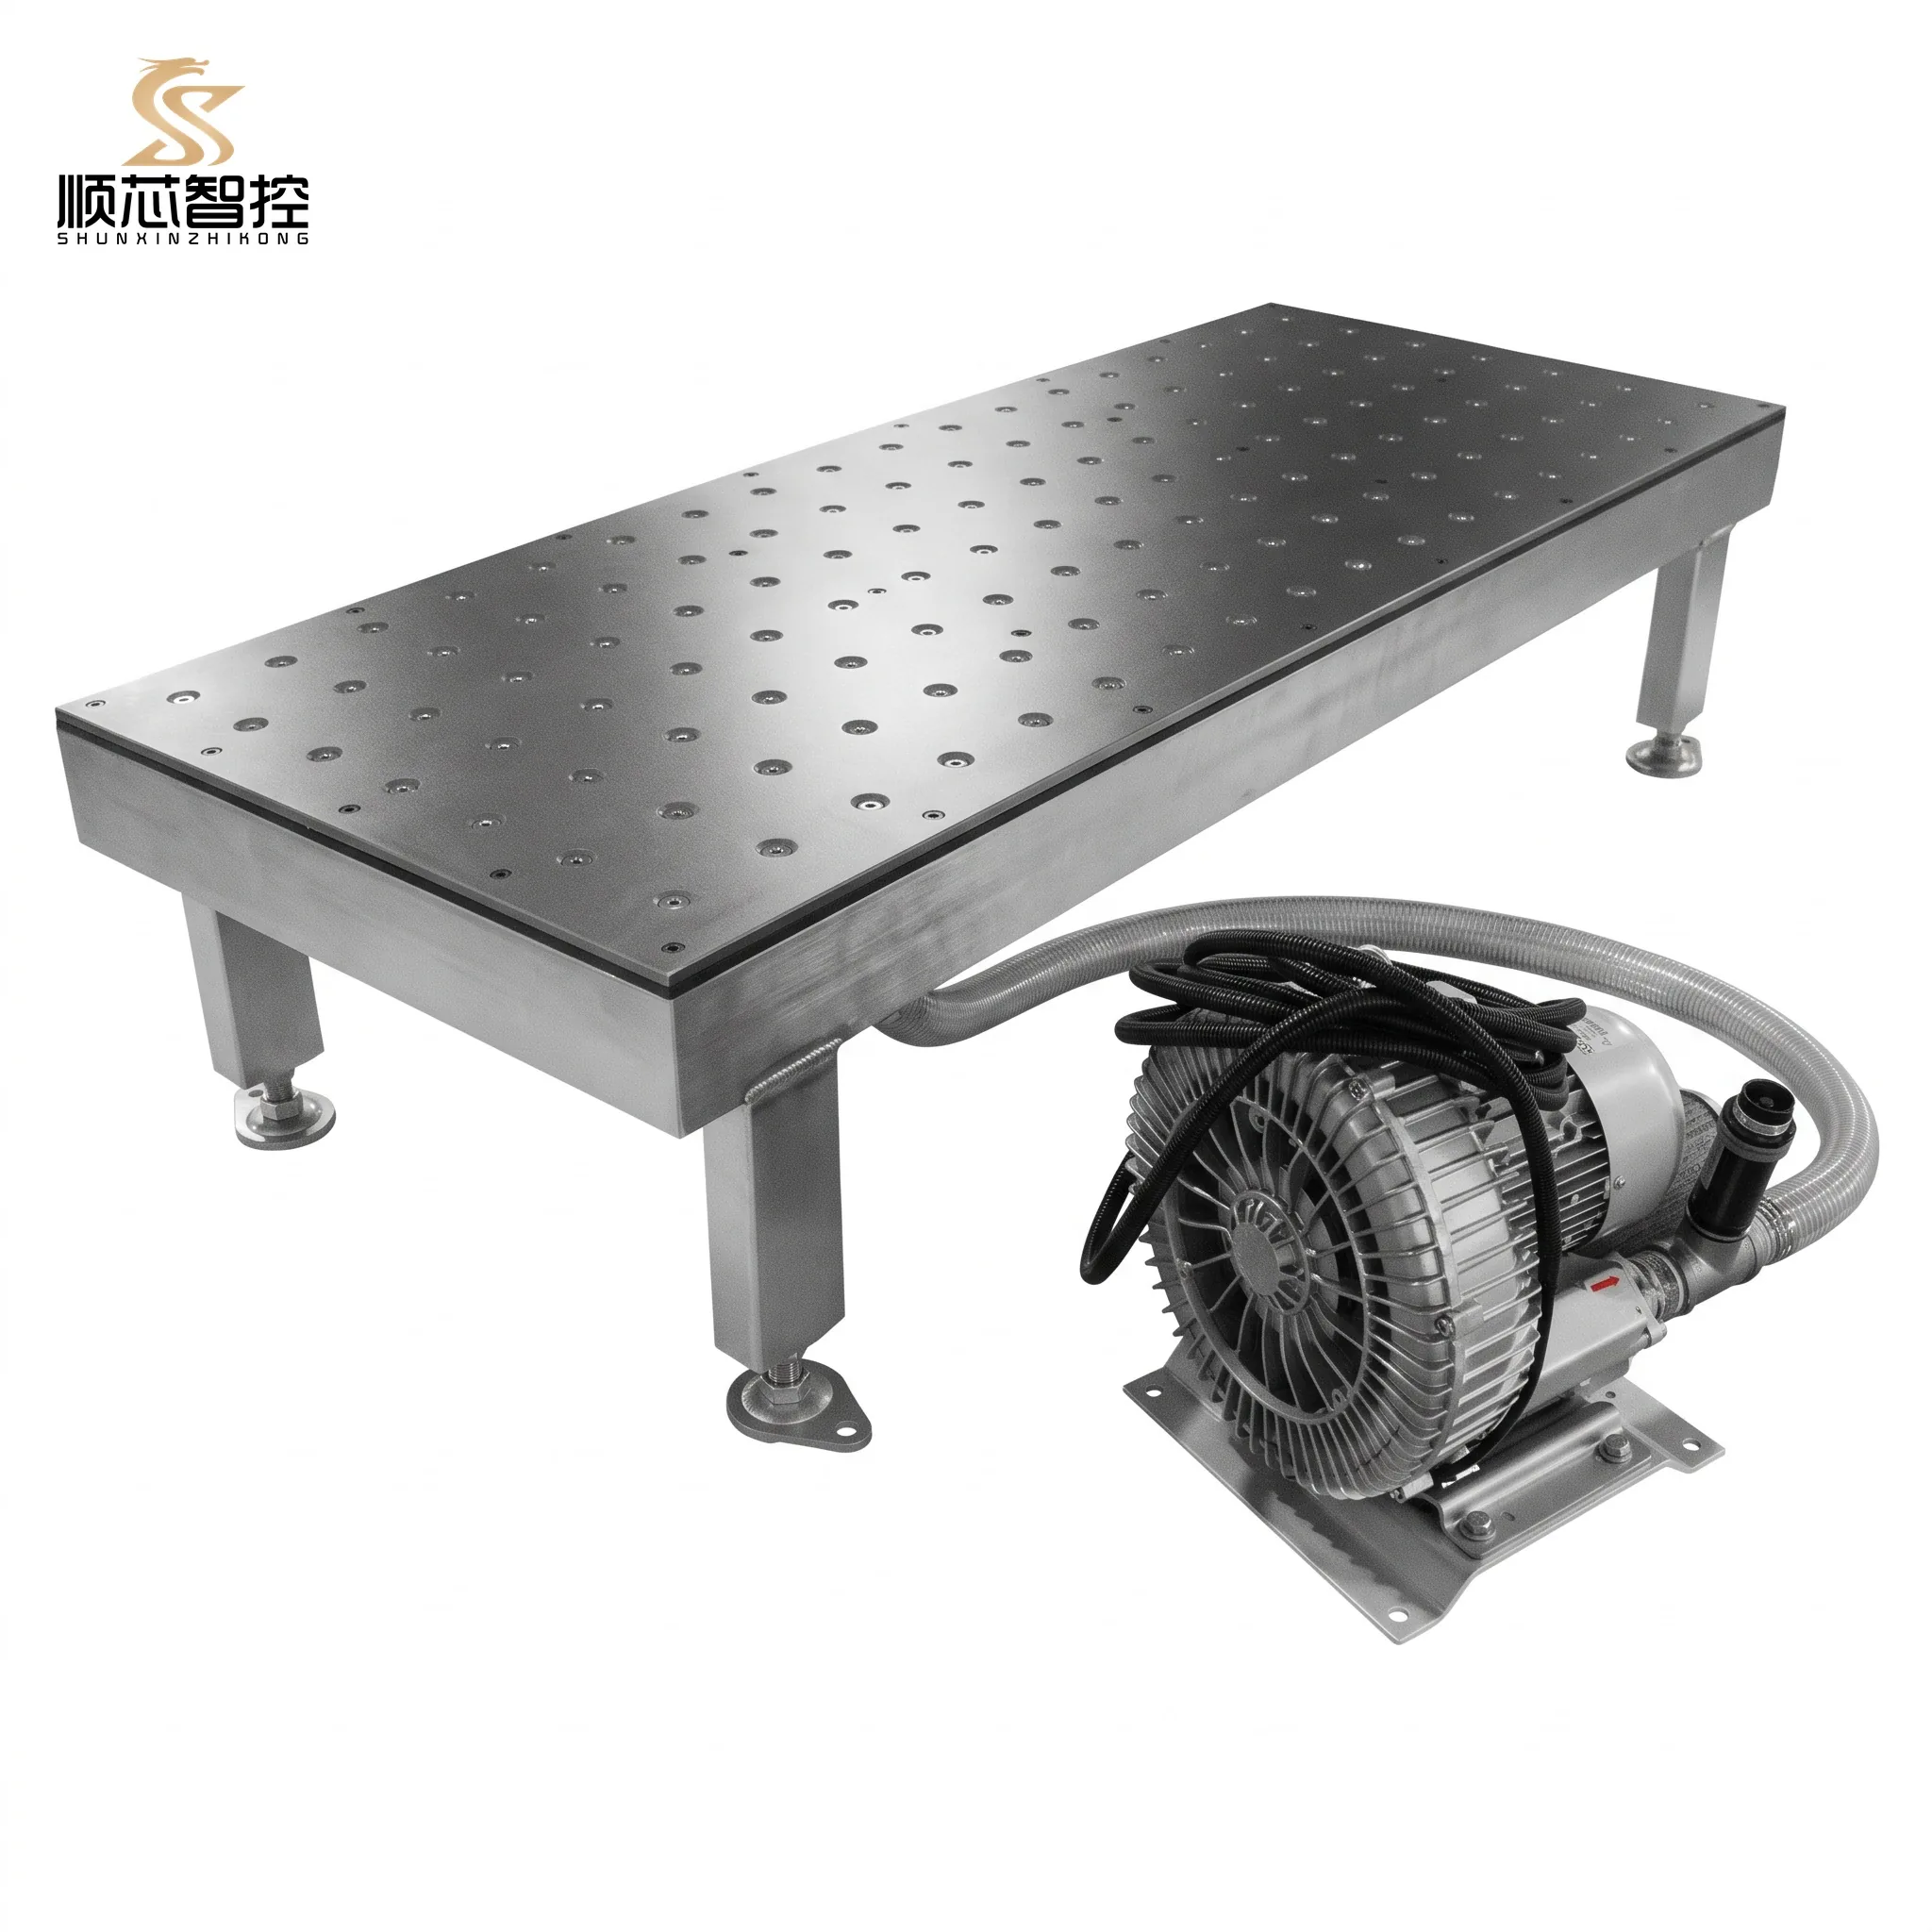
Heavy-duty centrifugal air blowers generate a continuous 0.5 mm pneumatic cushion. Spring-loaded phenolic or stainless steel ball valves float boards with near-zero friction.
4 Engineered Solutions to Achieve Zero-Defect Handling
Full Air-Flotation Transfer at Machine Infeed & Outfeed
Replace solid metal or bare caster tables with high-pressure air flotation tables. Pressurized clean air discharges only when the ball valve is depressed by board weight, creating a frictionless air film that prevents any direct contact between panel faces and table steel.
Automated Continuous 180° Belt Flippers
Eliminate manual board flipping. Continuous belt flippers clamp panels between top and bottom soft elastomeric belts, rotating the workpiece 180° in 12 seconds with zero sliding friction and zero point-pressure marks.
Electrostatic Neutralization Air Knives
Mount ionizing air bars immediately after the edge bander scraping and buffing stations. Neutralizing static electricity prevents ambient sawdust and plastic trim shreds from bonding to acrylic surfaces.
Polyurethane Roller Sleeves (Shore A 65-70)
Cover all return conveyor rollers with non-marking, vulcanized polyurethane sleeves. Polyurethane cushions minor board flexure and will not shed carbon black or leave track scuffs.
Global Industrial & GEO Export Standards for High-Gloss Processing
Premium cabinet export manufacturers operate under strict international criteria:
GEO STANDARDS High-Gloss Handling Compliance Matrix
- Electrical Standards: UL 508A certified panels, 480V 60Hz 3-Phase standard
- Safety Guarding: ANSI B11.19 compliant safety enclosures on all turnover machines
- Cost Offset: High replacement board costs (\$65/panel) provide full payback in under 2.8 months
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-emerald-400"></span>
European Union (Italy, Germany, Poland Luxury Kitchens)
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Directives: CE Machinery Directive 2006/42/EC, EN ISO 13849-1 Cat.3 / PL d safety relays</li>
<li>Optical Quality: Meets DIN 68861-4 scratch resistance surface criteria post-handling</li>
<li>Motors: IE3 premium efficiency variable-frequency drives with low noise emission (<70 dB)</li>
</ul>
</div>
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-amber-400"></span>
Middle East (UAE, Saudi Arabia Modern Interior Projects)
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Environment: High ambient temperature motor ratings (Class F insulation, IP55 enclosure)</li>
<li>Dust Control: Positive-pressure electrical cabinets prevent desert dust infiltration</li>
<li>Production Demand: Engineered for high-speed continuous multi-shift villa project processing</li>
</ul>
</div>
<div class="p-3 rounded-xl bg-slate-900 border border-slate-800/80">
<div class="font-bold text-white mb-1 flex items-center gap-2">
<span class="w-2 h-2 rounded-full bg-purple-400"></span>
Export Packaging & Sea Transit Standards
</div>
<ul class="space-y-1 text-slate-400 list-disc list-inside">
<li>Fumigation: Solid timber crates compliant with ISPM-15 international export regulations</li>
<li>Protection: High-grade VCI vapor corrosion inhibitor packaging with shock sensor tags</li>
<li>Container Fitting: Compact footprint modules fit standard 20GP / 40HQ container access</li>
</ul>
</div>
Technical Comparison: Surface Protection Methods
| Surface Handling Technology | Solid Steel Table Top | Standard Rubber Roller Bed | Centrifugal Air-Flotation Table | Automated 180° Belt Turnover |
|---|---|---|---|---|
| Direct Surface Contact Pressure | High Friction Metal Drag | Line Contact Pressure | Near-Zero (0.5mm Air Gap) | Uniform Distributed Soft Belt |
| Scratch Risk on Acrylic / PET | Extreme (>8% defect rate) | Moderate (1.5% defect rate) | Near-Zero (<0.05% defect rate) | Zero Scuff / Zero Denting |
| Handling Ergonomics | High Physical Effort | Medium Push Force | Fingertip 360° Gliding | 100% Unmanned Automatic Inversion |
| Max Panel Weight | 50 kg (Requires 2 workers) | 40 kg (Manual guiding) | Up to 100 kg / Panel | Up to 150 kg (Heavy Fire Doors) |
| Noise Level | Silent | Silent | Low Whispering Blower (<68 dB) | Smooth Servo Motion (<65 dB) |
Expert Quality Pro-Tips
[!TIP] Check Protective Film Integrity Before Trimming: High-gloss acrylic panels arrive from laminate presses with polyethylene (PE) protective films. Ensure the edge bander’s infeed fence does not peel film corners back. If film corners roll up during infeed, trimming knives can snag the plastic, dragging burrs across the board face.
[!WARNING] Never Clean Air Tables with Abrasive Solvent Compounds: Clean the phenolic air cushion bed with isopropyl alcohol and a microfiber cloth weekly. Never use solvent thinners or wire brushes, which can strip smooth epoxy bed coatings and clog ball check valves.
Technical Consultation & Plant Layout Support
Protecting high-gloss surfaces is essential to maintaining profitability in custom cabinet and modern door manufacturing. By replacing manual flipping with air-cushion gliding and synchronized belt turnover systems, workshops eliminate defects, protect operator health, and achieve predictable delivery schedules.
Contact our surface handling engineering specialists today with your board dimensions, coating types, and factory floor plan for customized CAD integration drawings and competitive CIF quotations.
All automated loop return procedures and electrical sensor alignments must adhere to standard workshop lockout-tagout (LOTO) protocols and host machinery manufacturer guidelines. Shunxin equipment includes universal dry-contact interlocks to ensure immediate emergency stop response across synchronized production lines.
Need a Custom Layout Drawing & Quotation for Your Workshop?
Send us your workshop dimensions or CAD floor plan. Our mechanical engineers will deliver a synchronized layout proposal and payback calculation within 24 hours.